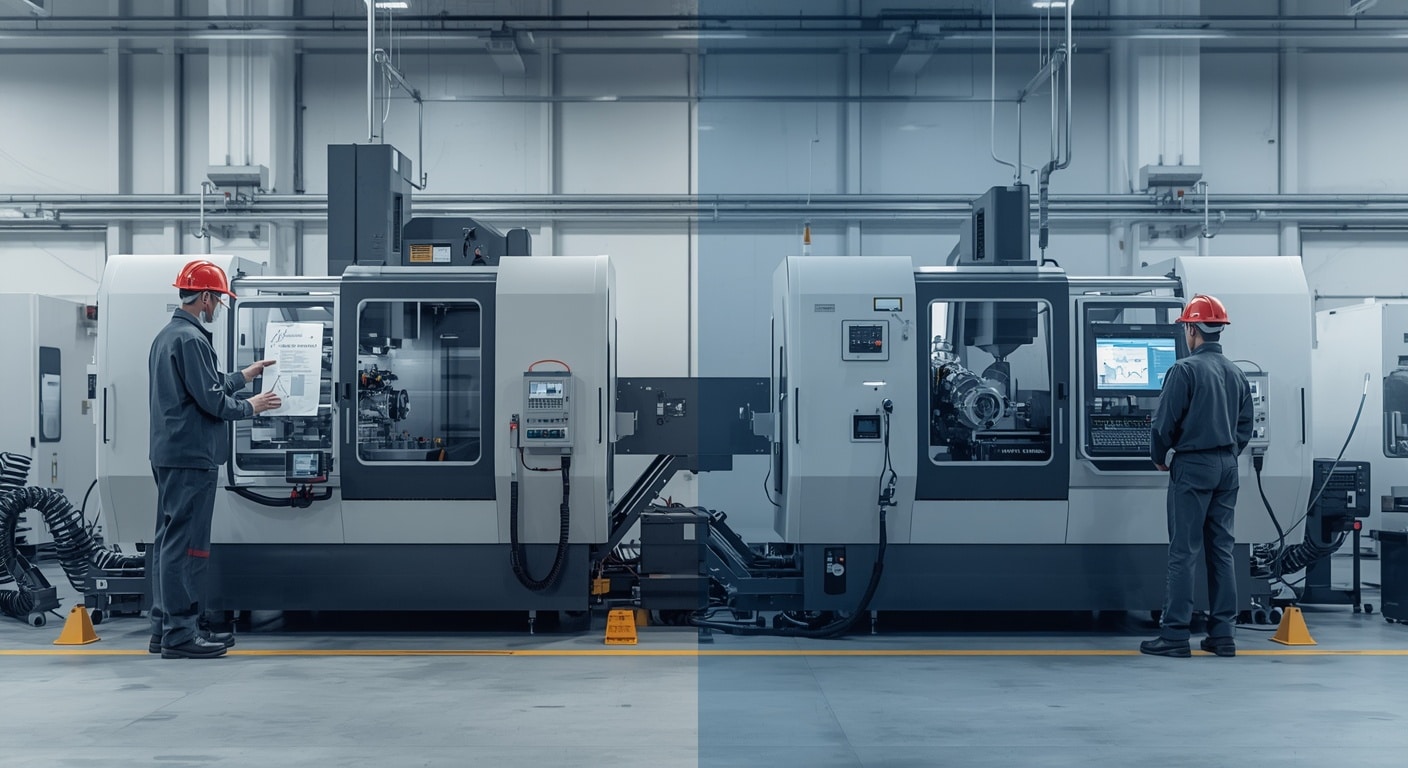
Preventive vs predictive maintenance is a common comparison for manufacturers trying to reduce breakdowns, control downtime and improve asset reliability. The two approaches share the same goal, but they work differently. Preventive maintenance follows a planned schedule, while predictive maintenance uses equipment condition data to decide when maintenance is actually needed. Understanding that difference helps factories choose a maintenance strategy that fits their machines, people and production priorities.
For most manufacturers, the choice is not simply about adopting the newest method. It is about matching the maintenance approach to asset criticality, operating conditions, internal capability and budget. In practice, many factories use a mix of both.
If you are reviewing maintenance planning as part of broader factory improvement, this factory operations and production management guide provides wider context on production systems, planning and operational control.
What Is the Difference Between Preventive and Predictive Maintenance?
Preventive maintenance is scheduled servicing carried out at set time, usage or cycle intervals to reduce the chance of failure. Predictive maintenance is condition-based maintenance that uses equipment data such as vibration, temperature or oil condition to indicate when maintenance should be performed before a likely failure occurs.
The main difference is timing. Preventive maintenance assumes service is needed according to a plan, while predictive maintenance aims to act according to the actual health of the asset. That distinction affects labour planning, downtime, tooling, spare parts management and the level of data required.
What Preventive Maintenance Means in a Factory Setting
Preventive maintenance is a planned maintenance approach built around routine tasks performed before obvious failure occurs. In a factory, the schedule is usually triggered by one or more of the following:
- Calendar intervals, such as weekly, monthly or quarterly checks
- Machine running hours
- Production cycles
- Output volume
- Manufacturer recommendations where appropriate
Typical preventive maintenance work includes lubrication, filter replacement, alignment checks, tightening, belt inspection, cleaning, calibration checks and scheduled replacement of wear parts. The objective is to keep industrial equipment in a stable operating condition and reduce avoidable stoppages.
For example, a factory may schedule conveyor inspections every month, replace air filters at fixed intervals, or lubricate bearings after a defined number of machine hours. None of these tasks depend on advanced sensor data. They depend on discipline, documentation and maintenance scheduling.
This is one reason preventive maintenance remains common in manufacturing. It is relatively easy to understand, easier to roll out across many assets and often suitable for equipment with predictable wear patterns. It also works well where failure modes are well known and the consequences of brief scheduled downtime are manageable.
Preventive maintenance is often the starting point for improving factory maintenance planning because it creates structure. Even a simple checklist and work order system can improve consistency compared with purely reactive maintenance.
What Predictive Maintenance Means in a Factory Setting
Predictive maintenance is a condition-based maintenance approach that relies on monitoring the actual state of equipment. Instead of replacing components or servicing machines purely by schedule, the maintenance team looks for signs that performance or condition is changing in a way that suggests a developing problem.
Common inputs can include:
- Vibration analysis
- Temperature trends
- Pressure readings
- Oil analysis
- Thermal imaging
- Sensor data from connected equipment
In practical terms, predictive maintenance asks a different question from preventive maintenance. Instead of asking, “Has it been three months since the last service?” it asks, “What is the machine telling us about its condition right now?”
For example, if a motor begins showing unusual vibration, rising heat or a change in lubrication condition, the maintenance team may investigate and plan intervention before the asset fails. The goal is not to wait until breakdown. It is to use condition monitoring to identify a developing issue early enough to act in a controlled way.
Predictive maintenance can be especially valuable for critical assets where unexpected downtime disrupts production planning, quality or delivery performance. However, it depends on having suitable data, a way to review that data and enough team capability to interpret what it means.
Preventive vs Predictive Maintenance: Key Differences
| Area | Preventive Maintenance | Predictive Maintenance |
|---|---|---|
| Maintenance timing | Based on fixed time, usage or cycle intervals | Based on asset condition and monitored trends |
| Information required | Basic maintenance history and schedule | Condition data, monitoring results and analysis |
| Setup complexity | Lower and easier to standardize | Higher due to tools, monitoring and interpretation |
| Cost profile | Usually simpler to start, but may lead to unnecessary servicing | Often higher to implement, but may reduce avoidable maintenance on critical assets |
| Skill requirements | Routine maintenance planning and execution skills | Condition monitoring, analysis and decision-making skills |
| Downtime profile | Planned downtime at scheduled intervals | Maintenance can be timed closer to actual need if data is reliable |
| Best fit | Stable, lower-risk or widely used assets | Critical, failure-sensitive or variable-condition assets |
| Scalability | Easier to apply across many standard machines | Usually best introduced selectively, then expanded |
These differences matter because the right equipment maintenance strategy depends on the type of asset and the cost of failure.
Timing
Preventive maintenance follows the calendar or usage meter. Predictive maintenance follows evidence from the equipment itself. If a part is still performing well, predictive methods may allow it to remain in service longer. If a problem appears earlier than expected, predictive methods may trigger earlier action.
Data needs
Preventive systems can run with basic maintenance records and a checklist. Predictive systems need condition monitoring inputs and a process for reviewing them. Without trustworthy data, predictive maintenance becomes guesswork rather than a disciplined method.
Implementation effort
Preventive maintenance is generally easier to establish because tasks and intervals can be defined in advance. Predictive maintenance requires more preparation, such as selecting critical assets, setting up monitoring points and deciding how findings will lead to work orders.
Downtime and maintenance timing
Preventive maintenance creates planned downtime even when the asset may still be healthy. Predictive maintenance aims to perform work nearer to actual need, which can improve machine downtime reduction when applied to the right equipment.
Suitability
Not every machine justifies predictive tools. Standard utility equipment or low-impact assets may be better managed through preventive routines. Critical rotating equipment, process bottlenecks or machines with costly failure consequences are often better candidates for predictive monitoring.
Advantages of Preventive Maintenance
Preventive maintenance remains widely used because it offers practical benefits that fit many factory environments.
Easier planning and scheduling
Because tasks are scheduled in advance, maintenance teams can coordinate labour, shutdown windows and spare parts more easily. This supports production planning and makes it simpler to communicate with operations teams.
Simpler to implement
A preventive maintenance programme does not require advanced predictive maintenance sensors or complex data analysis from the start. Many factories can begin with asset lists, basic checklists and planned intervals, then improve over time.
Useful for stable and predictable assets
Where failure patterns are relatively well understood, scheduled maintenance can be effective. Routine assets such as fans, conveyors, compressors, pumps or utility systems often benefit from consistent inspection and servicing.
Better consistency across teams
Standard work instructions make it easier to ensure tasks are not missed when staffing changes occur. This is particularly useful in multi-shift operations where machine care needs to be consistent.
Suitable for smaller factories
For SMEs and growing manufacturers, preventive maintenance can deliver meaningful control without major technology investment. A well-run planned maintenance system is usually far better than waiting for breakdowns and reacting under pressure.
Supports a maintenance culture
Even when a factory eventually adds predictive methods, preventive maintenance creates the discipline needed for better asset reliability. It encourages record-keeping, routine inspection and clearer ownership of equipment condition.
Advantages of Predictive Maintenance
Predictive maintenance can offer strong benefits when it is applied to the right assets with the right support.
Potentially reduces unplanned downtime
By identifying developing faults before failure, predictive maintenance can help maintenance teams intervene before a line-stopping event occurs. This is especially valuable where downtime has major production or delivery consequences.
Improves maintenance timing
One of the main advantages of predictive maintenance is that work can be performed closer to actual need. That may help avoid both late intervention and unnecessary early replacement.
Helps prioritize critical equipment
Not all assets have equal impact on output. Predictive methods make it easier to focus attention on machines that affect throughput, quality or safety of operations if they fail unexpectedly.
Can reduce unnecessary maintenance activity
When condition data shows that equipment remains healthy, maintenance may be deferred within a controlled decision process. This can reduce over-maintenance and allow labour to be used more selectively.
Supports better failure analysis
Trend data from vibration analysis, thermal imaging or lubricant condition can improve understanding of how assets deteriorate. Over time, that can strengthen the overall maintenance strategy for manufacturing and improve decision-making.
Improves visibility for reliability work
Predictive maintenance often supports a broader reliability mindset. Instead of simply completing scheduled tasks, the team begins to track patterns, identify recurring issues and connect maintenance findings to downtime, OEE and production loss.
These benefits are not automatic. Results depend on choosing suitable targets, making sure data is usable and ensuring someone in the maintenance team can turn findings into timely action.
Limitations and Challenges of Each Approach
Neither maintenance approach is perfect. The practical question is not which one sounds better, but which limitations are acceptable for a given asset or operation.
Limitations of preventive maintenance
- Over-maintenance: Parts may be replaced too early simply because the schedule says so.
- Unnecessary downtime: Machines may be stopped for planned work even when condition is still acceptable.
- Labour inefficiency: Teams may spend time on low-value routine tasks while more important issues build elsewhere.
- Not ideal for variable conditions: If equipment wear depends heavily on load, environment or operating pattern, a fixed schedule may be too early or too late.
Preventive maintenance works best when service intervals are reviewed periodically rather than treated as permanent.
Limitations of predictive maintenance
- Higher setup complexity: The factory needs monitoring methods, data capture and a response process.
- Training needs: Condition data has limited value if nobody can interpret it correctly.
- Selective applicability: Some assets do not justify the effort or do not produce useful condition signals.
- Process discipline required: If abnormal readings are collected but not acted on, the system fails operationally.
Predictive maintenance is also vulnerable to poor implementation. Installing tools without defining alarm response, maintenance ownership or follow-up work orders can create data without results.
Shared challenge: execution quality
Whether a factory uses preventive maintenance or predictive maintenance, the biggest weakness is often not the strategy itself but inconsistent execution. Missed inspections, poor maintenance records, delayed repairs and weak spare parts management can undermine either model.
How to Choose the Right Maintenance Strategy
The best approach is usually based on asset importance, failure risk and the factory’s readiness to support the method. Use this framework to choose between preventive and predictive maintenance.
- List your key assets. Start with a clear asset register that identifies machines, utilities and support equipment involved in production.
- Rank asset criticality. Ask which machines would stop production, affect product quality or create major disruption if they failed unexpectedly.
- Review failure history. Look at breakdown patterns, recurring faults, frequent part replacements and previous downtime events.
- Assess failure consequences. Consider whether failure leads mainly to minor inconvenience or to serious production loss, scrap, missed delivery or high repair urgency.
- Check data availability. Determine whether the asset has condition signals that can realistically be monitored, such as vibration, temperature, pressure or lubricant condition.
- Evaluate internal capability. Consider whether your maintenance team has the skills, time and processes to collect and use condition data properly.
- Compare cost and complexity. Do not focus only on technology cost. Also consider planned downtime, labour use, spare parts consumption and disruption from unexpected failure.
- Choose a mixed strategy where appropriate. Put lower-risk assets on preventive schedules and apply predictive monitoring to critical assets where it will make a meaningful difference.
- Review and adjust. Maintenance strategy should not remain static. Intervals, monitoring methods and priorities should be revised as equipment behaviour becomes clearer.
In most factories, the answer is not all preventive or all predictive. It is a layered equipment maintenance strategy based on criticality and evidence.
When a Hybrid Maintenance Approach Makes Sense
Many manufacturers get the best results from a hybrid maintenance model. In this approach, preventive maintenance remains the foundation, while predictive maintenance is applied selectively to higher-value or higher-risk assets.
For example, a factory may keep routine preventive maintenance schedules for general utility equipment, standard conveyors or non-critical motors, while using condition monitoring on assets that are more likely to cause major disruption if they fail unexpectedly.
A hybrid approach often makes sense when:
- The factory wants better machine downtime reduction without trying to monitor every asset
- Some equipment is critical while other equipment is easy to repair or replace
- The maintenance team is building capability gradually
- Budget allows targeted predictive tools but not plant-wide rollout
- Production planning requires tighter control over selected bottleneck machines
Examples of assets that may be separated in this way include pumps, compressors, motors, conveyors and CNC-related support equipment. The exact split depends on how each asset affects output, quality and recoverability after failure.
This hybrid model is often more realistic than treating predictive maintenance as a complete replacement for preventive schedules. In practice, even condition-based systems still rely on good planning, inspections, work orders and execution discipline.
Practical Examples for Manufacturers and SMEs
Example 1: Small factory using preventive maintenance for standard equipment
A small manufacturer with limited maintenance resources may use preventive maintenance for air systems, conveyors and packaging equipment. The team follows a calendar-based checklist for lubrication, inspection, cleaning and replacement of common wear items. This controls breakdown risk without needing advanced monitoring tools.
Example 2: Larger plant using predictive monitoring for critical rotating assets
A larger plant may identify a small number of rotating assets that have a high impact on uptime. For these machines, the maintenance team tracks vibration, temperature or lubricant condition and plans intervention when trends show deterioration. Less critical equipment remains on routine planned maintenance.
Example 3: Mixed approach for cost control
A factory with moderate budget constraints may keep most machines on preventive maintenance but introduce predictive methods only for assets that frequently create urgent downtime. This allows better targeting of resources without attempting a full digital maintenance rollout.
Example 4: SME building toward predictive maintenance gradually
An SME may begin by improving maintenance scheduling, documenting recurring failures in a CMMS and reviewing downtime trends. Once the team understands which machines are truly critical, it can add condition monitoring selectively instead of investing broadly from the start.
Implementation Tips for Better Maintenance Results
Regardless of which approach you prefer, maintenance performance usually improves when the basics are handled well.
- Build a complete asset list. Make sure all important production and support equipment is identified clearly.
- Rank critical equipment. Separate true production-critical assets from lower-impact equipment.
- Document recurring failures. Record what fails, how often, under what conditions and how long recovery takes.
- Set maintenance intervals deliberately. Do not copy schedules blindly. Review whether intervals match actual operating conditions.
- Use a CMMS where practical. Even a simple system can improve work order control, maintenance history and checklist consistency.
- Coordinate with production planning. Scheduled maintenance is more effective when it aligns with planned stoppages and capacity needs.
- Review spare parts management. Critical spares should be identified so planned work does not become delayed reactive work.
- Track downtime trends. Look for patterns by asset, failure type and frequency to improve your maintenance strategy over time.
- Train for execution, not just theory. Teams need to know how to inspect, report and act on findings consistently.
- Start small and expand based on results. This is especially important for predictive maintenance, where selective early wins often matter more than wide rollout.
Manufacturing maintenance best practices are often less about adopting a single method and more about combining planning, discipline, asset knowledge and continuous review.
Conclusion: Preventive vs Predictive Maintenance for Manufacturing
When comparing preventive vs predictive maintenance, the core difference is simple: preventive maintenance is performed on a schedule, while predictive maintenance is performed based on asset condition. Preventive maintenance is usually easier to implement and manage across many assets. Predictive maintenance can offer better timing and stronger focus on critical equipment when the factory has the right data and capability.
For many manufacturers, the most practical answer is not choosing one approach exclusively. It is building a maintenance strategy that uses preventive routines as a foundation and applies predictive methods where failure consequences justify the added effort. The right balance depends on criticality, downtime impact, data readiness, internal skills and operational goals.
Frequently Asked Questions
Is preventive maintenance better than predictive maintenance?
Neither is universally better. Preventive maintenance is often better for simpler implementation and broad asset coverage, while predictive maintenance is often better for critical assets where condition data can improve maintenance timing. The best choice depends on risk, budget and asset importance.
What types of equipment are best suited to predictive maintenance?
Predictive maintenance is usually best suited to critical equipment where failure has a strong effect on production, quality or recovery time, and where useful condition signals can be monitored. Rotating assets and bottleneck machines are common candidates, but selection should be based on actual criticality and data value.
Can small manufacturers use predictive maintenance without a large budget?
Yes, if they apply it selectively. Small manufacturers do not need to monitor every machine. A practical approach is to strengthen preventive maintenance first, identify a few critical assets and add simple condition monitoring only where it supports better decisions.
Why do some factories use both preventive and predictive maintenance?
Factories often use both because different assets need different levels of control. Preventive maintenance is efficient for routine equipment, while predictive maintenance is more useful for selected critical machines. A hybrid model helps control cost while improving reliability where it matters most.
How often should preventive maintenance schedules be reviewed?
Preventive maintenance schedules should be reviewed regularly, especially after recurring failures, major process changes, altered production loads or evidence that tasks are being done too early or too late. Review frequency varies by operation, but intervals should not remain unchanged if actual equipment behaviour suggests otherwise.