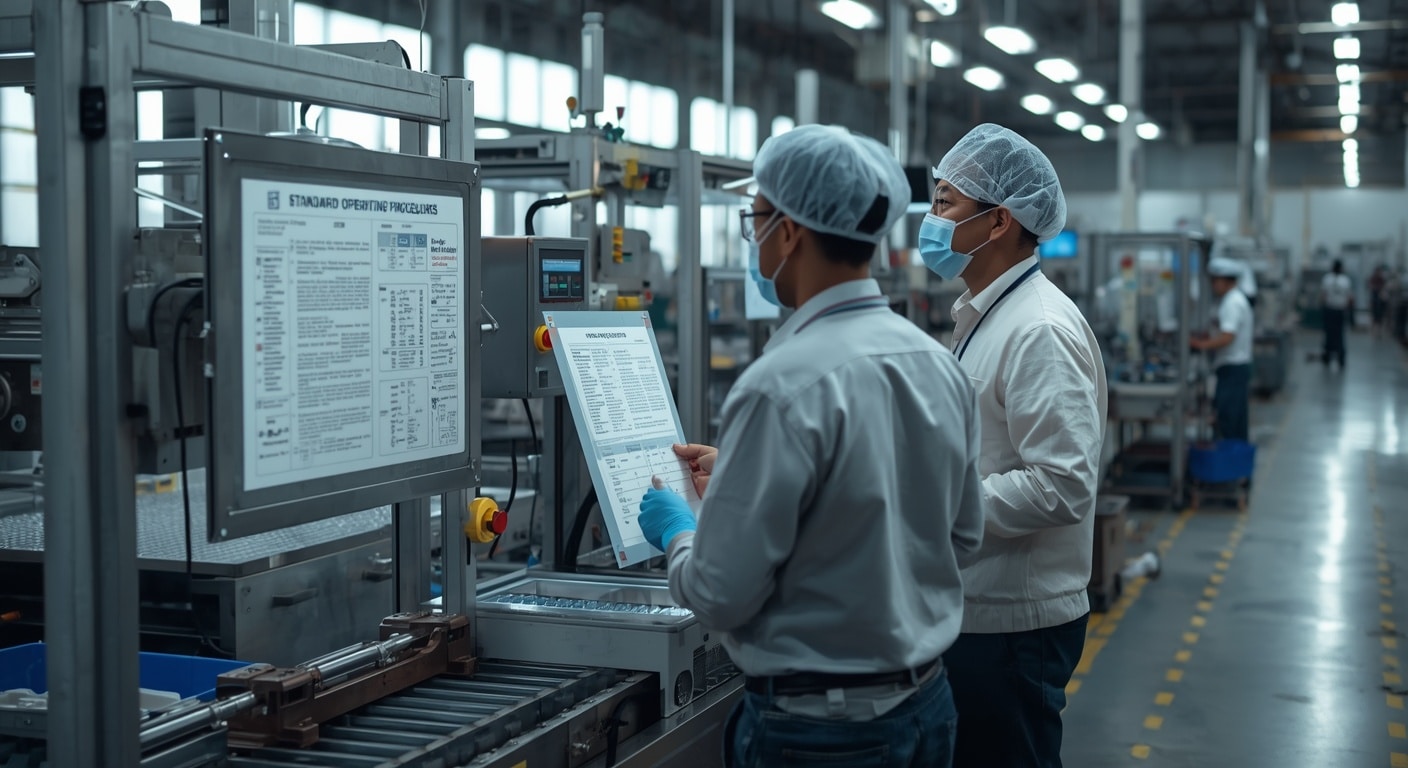
Factory standard operating procedures are one of the most practical tools for improving consistency on the shop floor. In manufacturing, recurring tasks such as machine startup, material handling, inspection, cleaning and shift handover should not depend only on memory or individual habits. Clear documented procedures help factories perform work more safely, more consistently and with fewer avoidable variations.
This guide explains what factory SOPs are, where they are used, what a good manufacturing SOP should include, and how to create procedures that operators and supervisors can actually follow. It also covers the difference between SOPs and work instructions, common implementation mistakes, and the basics of document control.
For broader operational context, readers can also refer to the Factory Operations & Production Management Guide.
What are factory standard operating procedures?
Factory standard operating procedures are documented instructions that standardize recurring factory tasks so they are carried out in a consistent, safe and controlled way. They are commonly used in production, maintenance, quality checks, cleaning, material handling and other routine operations where repeatability matters.
In simple terms, an SOP tells people how a process should be performed, who is responsible, what controls must be followed and what records may need to be completed. In manufacturing, this matters because even routine work can produce different results if each shift, operator or department follows a different method.
Standard operating procedures in manufacturing usually sit above day-to-day verbal instruction. They create a common reference point for production managers, shop floor supervisors, operators, maintenance personnel and quality teams. A well-written factory SOP is not just a file for audits. It is a working document that supports real operations.
Why SOPs matter in factory operations
SOPs matter because factories depend on repeatable processes. When the same task is performed in different ways, the result is often variation in output, quality, timing or safety practice. A documented procedure reduces that variation by setting out the expected method.
From an operations perspective, SOP implementation in factories can help with several day-to-day needs:
- Consistency: operators follow the same basic sequence for recurring tasks.
- Training: new employees have a documented reference instead of relying only on informal coaching.
- Quality control: key checks and acceptance points are less likely to be missed.
- Safety practice: important precautions, warnings and required controls can be included in the procedure.
- Shift handover: teams across shifts can follow the same expectations.
- Problem solving: when a process is documented, it is easier to identify where deviation occurred.
- Audits and reviews: managers can compare actual practice against the approved method.
Just as importantly, factory process standardization helps reduce confusion between departments. Production, quality, warehouse and maintenance teams often interact in the same workflow. If each team understands the approved process, coordination becomes easier.
That does not mean SOPs guarantee perfect execution. A procedure only works when it reflects the real process, is accessible to the people doing the work, and is supported by training and supervision.
Where SOPs are used in a factory
Shop floor procedures are useful anywhere work is repeated often enough that a standard method adds value. In many factories, SOPs are used across both production and supporting functions.
Production operations
Production SOPs commonly cover routine manufacturing activities such as line startup, shutdown, changeover, line clearance, in-process checks, packaging and end-of-shift closeout. These are tasks where sequence and discipline matter because skipped steps can affect quality, throughput or cleanliness.
Material receiving and storage
Operational procedures for factories also apply before production starts. Incoming material inspection, receiving documentation, storage conditions, identification labelling and stock movement can all benefit from clear steps. This helps warehouse teams and production teams work from the same expectations.
Quality inspection and handling of nonconforming items
Quality control activities often require a standard method so that checks are performed uniformly. For example, a factory may document how to sample, inspect, label, segregate or report items that do not meet internal requirements. The exact criteria may vary by product, but the process discipline can still be standardized.
Cleaning and housekeeping
Cleaning procedures are often underestimated, yet they affect safety, product quality and workplace organization. SOPs can define what needs to be cleaned, when it should be done, what materials or tools are used, and how completion is recorded where relevant.
Maintenance activities
Maintenance procedures may cover planned servicing, inspection routines, lubrication points, equipment checks, permit or escalation workflows, and restart coordination with production. For higher-risk tasks, the exact controls should reflect the factory’s verified safety requirements and equipment conditions rather than a generic template.
Incident reporting and escalation
Factories also use SOPs for communication and escalation. Examples include equipment abnormality reporting, product hold procedures, customer complaint handling support steps, and shift escalation when production cannot continue normally.
In short, if a task is repeated, affects quality or safety, involves several teams, or creates problems when done inconsistently, it is a strong candidate for an SOP.
What a good manufacturing SOP should include
A good manufacturing SOP should tell the right people exactly what the procedure covers, when it applies, how it is performed and what records or controls are required. It should be clear enough for consistent execution and structured enough for document control.
| Section | What it should cover |
|---|---|
| Title | A clear name for the procedure, such as production startup SOP or incoming material inspection SOP. |
| Purpose | Why the SOP exists and what operational issue it is meant to control or standardize. |
| Scope | Which process, line, machine, department, product family or activity the SOP applies to. |
| Responsibilities | Who performs the task, who checks it, and who approves or escalates issues. |
| Required tools or PPE | Any necessary tools, materials, forms or personal protective equipment, where applicable. |
| Step-by-step procedure | The sequence of actions to complete the task correctly. |
| Safety notes | Important warnings, precautions or task-specific controls that users must follow. |
| Quality checkpoints | Verification points, inspection steps or acceptance checks built into the process. |
| Records to complete | Logs, checklists, batch records, maintenance entries or other documents generated during the task. |
| Revision history | Version number, date of change and a short description of what was updated. |
| Approval details | Document owner and the functions responsible for review and approval. |
Not every SOP format for manufacturing will look exactly the same. A simple cleaning SOP may be shorter than a production changeover SOP. The key is not length. The key is whether the document gives users enough information to perform the task consistently and correctly.
SOP vs work instruction: what is the difference?
An SOP usually explains the standard process, purpose, scope and responsibilities for a recurring activity. A work instruction goes into more detailed task-level guidance for a specific operation, machine or method. In practice, an SOP says what the standard process is, while a work instruction shows exactly how to perform a particular task within that process.
| Aspect | SOP | Work Instruction |
|---|---|---|
| Main purpose | Standardize a process or recurring operational activity | Explain exactly how to perform a specific task |
| Level of detail | Moderate; process-oriented | Higher; task-oriented |
| Typical scope | Department, workflow, line activity or cross-functional process | Single job step, machine setting, inspection method or assembly action |
| Audience | Operators, supervisors, support functions and reviewers | The person directly performing the task |
| Content style | Purpose, scope, responsibilities, steps, checkpoints and records | Detailed sequence, settings, visuals, examples or exact handling method |
| Example | Line changeover SOP | Work instruction for changing a specific tooling set on one machine |
The distinction matters because some factories try to put everything into one document. That often leads to long, hard-to-use procedures. A better structure is to keep the SOP focused on the process and responsibilities, then attach or reference supporting work instructions where more detail is needed.
How to create factory standard operating procedures
Creating factory standard operating procedures works best as a structured process rather than a desk exercise. The goal is to document the safest and most consistent practical method currently approved by the factory.
- Select the process. Start with a recurring activity that affects quality, safety, output, coordination or training. Prioritize tasks where inconsistent execution causes real operational problems.
- Observe current practice. Review how the task is actually being done on the shop floor, not just how managers think it is being done. Note variations between shifts, lines or operators.
- Involve operators and supervisors. Speak to the people who perform and oversee the task daily. They often know where the process fails, where confusion occurs and which steps are essential.
- Document the best approved method. Write the procedure in a clear sequence. Include responsibilities, tools, precautions, quality checkpoints and records where relevant.
- Test the draft. Ask actual users to follow the draft SOP and identify unclear steps, missing information or impractical wording.
- Review and approve it. The appropriate process owner, supervisor or designated reviewer should confirm that the SOP reflects the approved method.
- Train staff. Explain the procedure to the people who use it. Do not assume that issuing the document alone means the process has been adopted.
- Control revisions. Assign a version number, remove obsolete copies from use, and update the SOP whenever the process changes or recurring issues show that the document is no longer accurate.
This process is more effective than copying manufacturing SOP examples from another site or industry. A borrowed template may help with structure, but the content must reflect the actual machine, workflow, people and controls in the factory using it.
How to make SOPs practical for the shop floor
Many SOPs fail not because the process is wrong, but because the document is difficult to use. If operators cannot quickly understand a procedure during real work, the SOP becomes a filing exercise rather than an operational tool.
Use plain language
Write instructions as directly as possible. Avoid long paragraphs, internal jargon that new staff may not understand, and policy-style wording that does not help someone perform the task. If a term must be used, define it clearly.
Keep the steps sequential
People follow procedures more reliably when the steps match the real order of work. If preparation, execution, verification and closeout are separate stages, show them in that order.
Specify responsibilities clearly
Do not write vaguely. State who does what. For example, if an operator performs the check, a supervisor verifies exceptions, and quality control releases the next stage, those roles should be visible in the procedure.
Use visuals where appropriate
Photos, diagrams, labels, machine part references or sample forms can make work instructions for factory operations easier to follow, especially for tasks with several similar-looking components or checkpoints.
Place the SOP where the task happens
If users need the document during the activity, it should be available near the relevant workstation, machine, line area or controlled digital access point. A procedure stored only in an office cabinet is less likely to influence actual behaviour.
Consider language needs
In Malaysian factories, workforces may include employees with different language preferences or literacy levels. Where appropriate, factories may need clearer visuals, simplified wording, translated support materials or supervisor-led training so the intended instructions are understood consistently. The exact approach depends on the workforce and task complexity.
Common mistakes when implementing SOPs in factories
Even well-intended SOP implementation in factories can break down if common mistakes are not addressed early.
Copying generic templates without adapting them
A template can help with document structure, but it cannot replace process knowledge. An SOP that does not match the actual line, product, workflow or equipment will quickly lose credibility with operators.
Practical fix: use templates only as a format. Build the content from real observation and internal process knowledge.
Writing procedures without operator input
Documents created only by office staff often miss practical details. Operators may know the real sequence, common errors, material handling issues or machine conditions that affect execution.
Practical fix: involve operators, technicians and shop floor supervisors during drafting and testing.
Confusing SOPs with policy documents
A policy states intent or rules. An SOP explains how work is done. When factories use broad policy language inside operational documents, users still do not know what sequence to follow.
Practical fix: keep policies and operational procedures separate. Use SOPs for actionable process guidance.
Overcomplicating the document
Some procedures become so detailed that users stop reading them. Others are too short and omit critical steps. The right balance depends on the task.
Practical fix: keep SOPs process-focused and link detailed work instructions where needed.
Failing to train people after issue
Issuing a new revision does not mean it has been understood. Without training, staff may continue following old habits.
Practical fix: connect document release with training, communication and supervisor follow-up.
Allowing outdated versions to remain in use
One of the most common factory documentation practices failures is version confusion. If old hard copies remain at workstations, teams may unknowingly follow obsolete instructions.
Practical fix: use clear version control, defined ownership and a method for removing superseded copies.
Reviewing, updating and controlling SOP documents
Writing an SOP is only the start. To stay useful, the document must remain accurate as equipment, processes, materials and responsibilities change. This is where document control becomes important.
Use version numbers and approval ownership
Each SOP should have a clear identifier or version number and an owner responsible for maintaining it. Approval responsibility should also be defined so users know which version is current and who authorized it.
Track what changed
When an SOP is updated, include a short revision note or change summary. This helps supervisors and users understand whether the change is minor formatting or something that affects how the job is done.
Review SOPs when the process changes
Scheduled periodic review can be useful, but review should also happen when there is a clear trigger. Common triggers include:
- process or layout changes
- new equipment or tooling
- material changes
- quality issues or repeated defects
- safety incidents or near misses
- customer requirement changes
- recurring operator confusion
The right review frequency depends on the complexity and risk of the process. Some SOPs may need more frequent review than others.
Control obsolete copies
Factories should have a practical method to prevent outdated SOPs from being used. This can include controlled issue points, removal of superseded copies, archive management and communication of new revisions to affected departments.
Retain related records sensibly
Training records, sign-off sheets, logs and related operational documents may need to be retained based on the factory’s internal system, customer requirements or applicable obligations. Exact retention periods should be confirmed by the business based on its actual legal, contractual or certification context rather than assumed from generic guidance.
Simple examples of factory SOP categories
Factories usually need more than one type of SOP. Different functions require different levels of documentation depending on process complexity, product type and operational risk.
- Production startup SOP: steps for preparing the line, confirming readiness, checking materials and beginning the run.
- Line clearance SOP: a standard method for confirming that the previous job, labels, materials or records have been cleared before the next job starts.
- Incoming material inspection SOP: how received items are identified, checked, recorded and accepted, held or escalated.
- Cleaning SOP: what must be cleaned, by whom, when, with what tools or materials, and how completion is confirmed.
- Maintenance procedure: routine servicing or inspection steps, including coordination between maintenance and production. For tasks involving hazardous energy or machine isolation, the exact controls should be defined using the factory’s verified safety requirements.
- Warehouse dispatch SOP: order picking, verification, packaging, loading checks and document handling before goods leave the site.
- Nonconforming product handling SOP: segregation, identification, review and escalation of items that do not meet the required condition.
These examples show categories rather than fixed templates. A food processor, electronics assembler and metal fabrication plant will not all document these processes in the same way. Their SOPs should reflect their actual products, process steps and risk profile.
How Malaysian manufacturers can approach SOPs responsibly
For Malaysian manufacturers, the most responsible approach is to make SOPs reflect the real operation rather than adopting generic documents for appearance. The right procedure depends on the factory’s products, equipment, workforce, layout, customer expectations and internal control needs.
This is especially important when SOPs touch on safety procedures, quality documentation or regulated product categories. Requirements can vary depending on industry, activity and the standards or customer systems a manufacturer works under. A procedure that suits one plant may be incomplete or inappropriate for another.
Factories should therefore verify any regulatory, customer, certification or industry-specific documentation requirements with the relevant authority, customer, certification body or qualified internal compliance owner before final adoption. That is a safer approach than assuming every manufacturing site must use the same SOP format or the same approval process.
In practice, responsible SOP management means:
- documenting the actual approved method used in the plant
- aligning procedures with real production and support workflows
- training users before expecting compliance
- keeping revision control disciplined
- reviewing procedures after change, incident or recurring quality issues
Conclusion: building SOPs that people actually follow
The best factory standard operating procedures are not the longest or most formal documents. They are the ones people can understand, access and use consistently during real work. That usually comes down to clear writing, operator involvement, practical formatting, training and disciplined document control.
For factory managers and operations teams, the priority is simple: standardize the tasks that matter, document the method that actually works, and keep the procedure accurate as the process changes. When SOPs are built around real shop floor use, they become a practical part of factory operations rather than just another document in the system.
Frequently Asked Questions
What are factory standard operating procedures used for?
Factory standard operating procedures are used to standardize recurring tasks such as production steps, inspections, cleaning, material handling, maintenance support and shift handovers. Their purpose is to improve consistency, clarify responsibilities, support training and reduce avoidable variation in how work is performed.
What is the difference between a factory SOP and a work instruction?
A factory SOP usually describes the overall process, scope, responsibilities and key steps for a recurring activity. A work instruction provides more detailed guidance for a specific task, machine, method or checkpoint within that process.
What should be included in a manufacturing SOP?
A manufacturing SOP should typically include a title, purpose, scope, responsibilities, required tools or PPE where relevant, step-by-step instructions, safety notes, quality checkpoints, records to complete, revision history and approval details.
Who should write and approve SOPs in a factory?
SOPs are usually drafted by people who understand the process well, often with input from operators, supervisors and relevant support functions such as quality or maintenance. Approval should come from the appropriate process owner or designated reviewer within the factory’s document control system.
How often should factory SOPs be reviewed and updated?
There is no single review interval that fits every SOP. Procedures should be reviewed periodically based on the factory’s internal system and also whenever there is a process change, new equipment, repeated quality issues, an incident, or evidence that the existing procedure no longer reflects actual practice.